Skip to content
Oldershaw Group
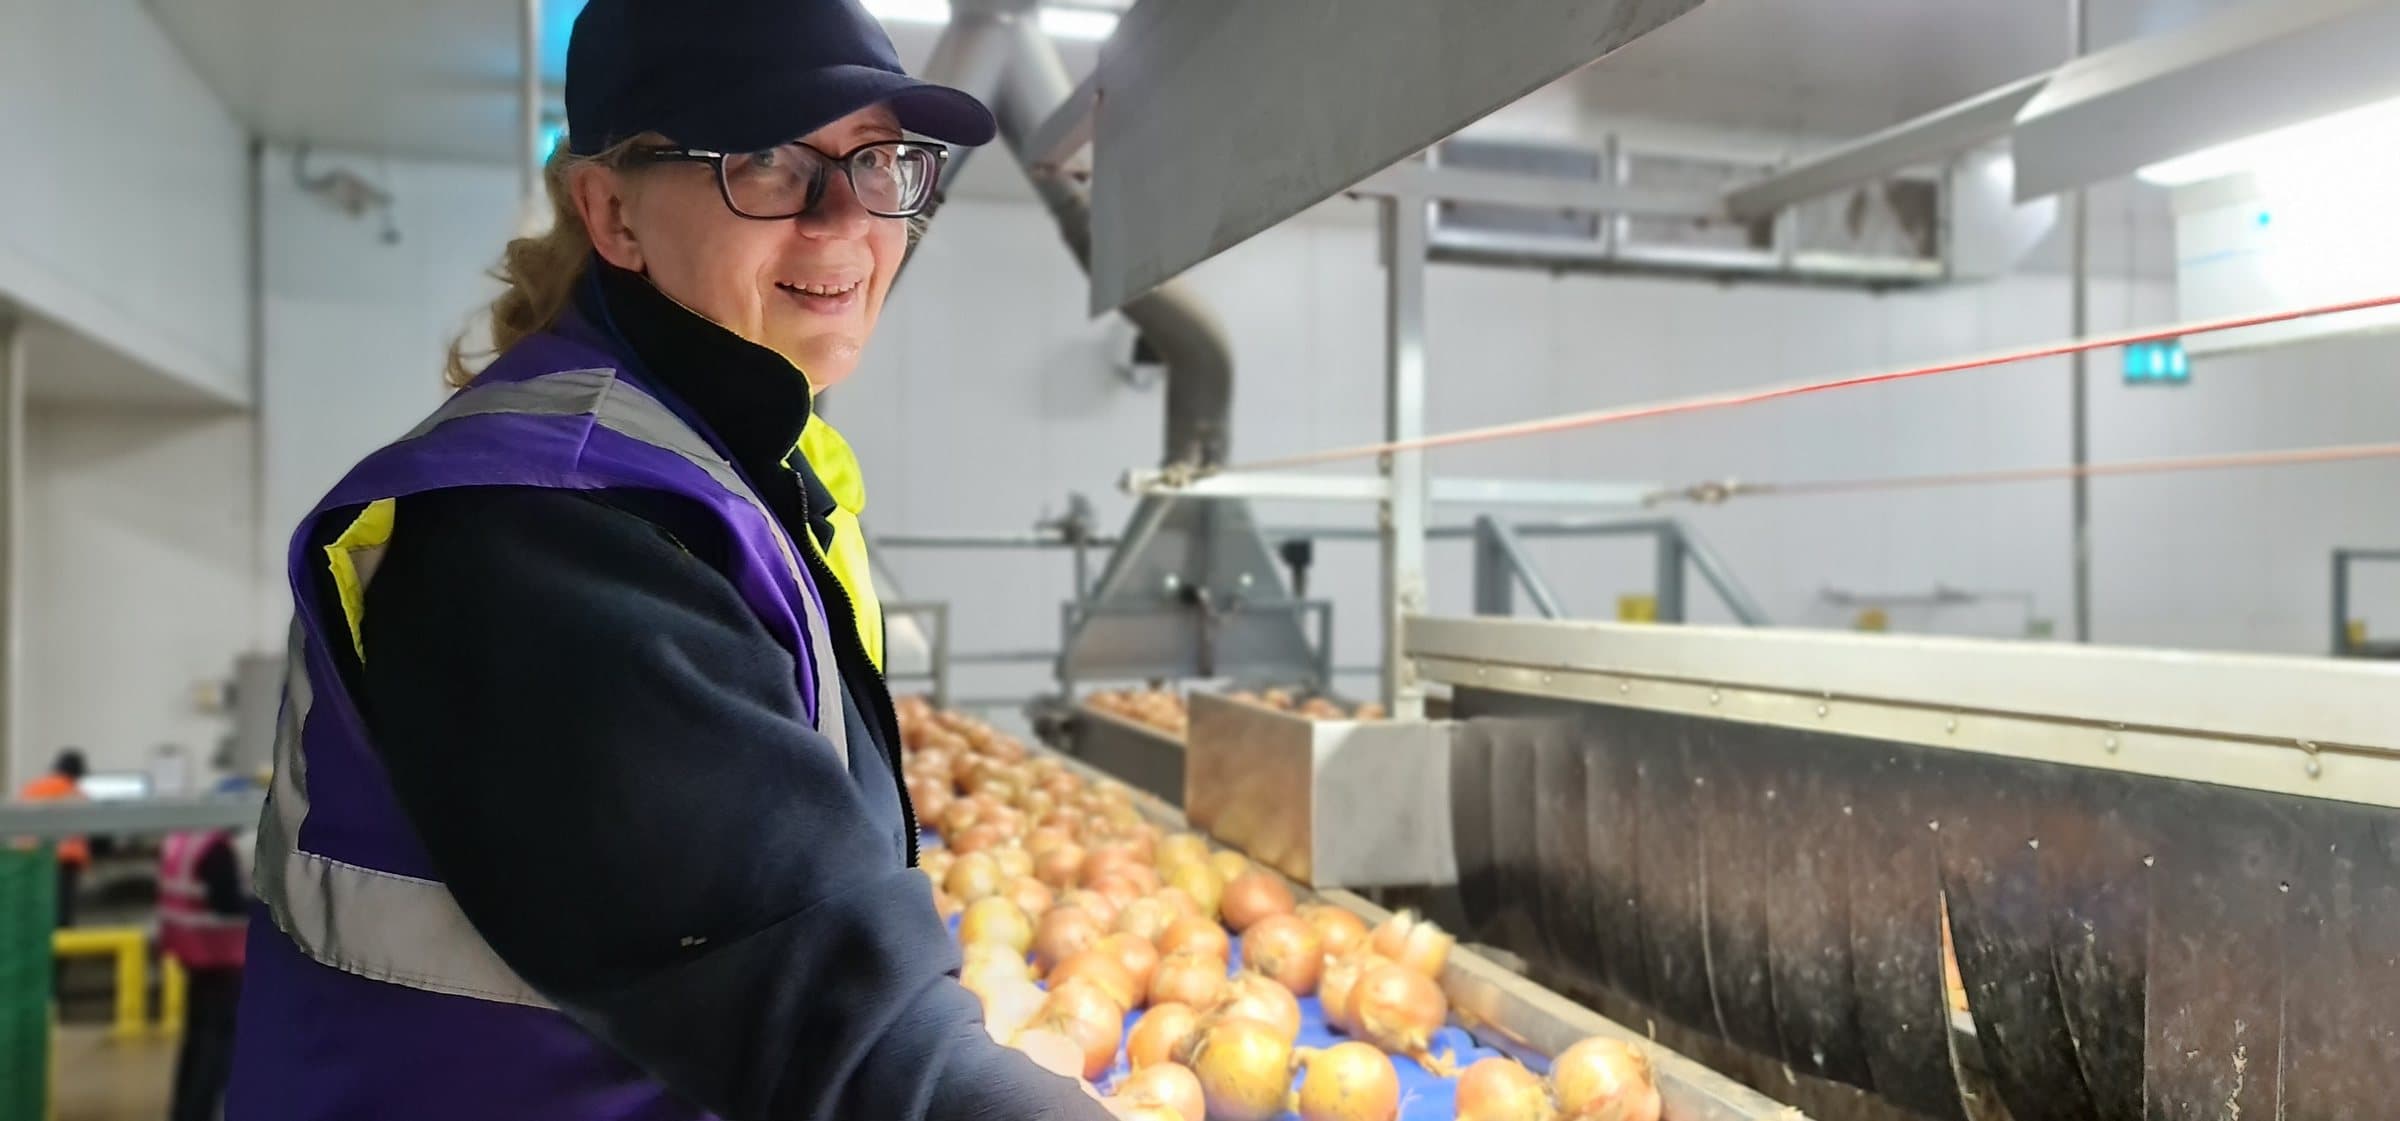
A colleague working alongside onions on the grading line in the Moulton packhouse

Careers at Oldershaw Group

We grow the best onions and shallots in Britain, and we do it as a family business that thinks in decades, not quarters. Join us and you get real ownership, work you can see the results of, and a front-row seat on the technology reshaping our industry.

11 open roles

Shift

Shift pattern

Engineering · Full Time, Permanent

Engineering Administrator

Days
29,000Monday to FridayShift times: 08:00 - 16:30

An Engineering Administrator to provide efficient administrative and stock control support to the Engineering team. The role ensures that purchasing, deliveries, stock records, paperwork, servicing information and engineering documentation are accurate, organised and kept up to date. The Position: • Create purchase orders for quotes and customer orders using Linkfresh. • Accurately record and maintain all purchase orders on the purchase order spreadsheet. • Issue purchase orders to the relevant suppliers and companies in a timely manner. • Update and sign off purchase orders once deliveries have been received or jobs completed, liaising with the Accounts Department to reconcile delivery notes and invoices. • Place stock and engineering orders as required, ensuring all necessary approvals are obtained. • Ensure all incoming deliveries are clearly labelled with the correct stock numbers. • Record incoming deliveries promptly and accurately on the stock spreadsheet. • Ensure all deliveries are stored in the correct stock locations. • Maintain accurate and up-to-date records of part numbers, stock quantities, storage locations and prices. • Update stock records to reflect parts that have been used or removed. • Regularly monitor stock levels and identify items requiring reordering. • Ensure all stock is stored correctly, securely and in a way that allows items to be located easily. • Ensure all boxes and storage locations are clearly and accurately labelled with the relevant part numbers. • Play an active role in developing and implementing a new, accurate and up-to-date stock management system. • Maintain and update the team planner, including promotions, projects, training and holidays, to support effective forward planning. • Maintain accurate records of team overtime and additional working days for payroll purposes. • Organise, update and maintain service plan sheets. • Ensure all relevant paperwork and documentation is complete, accurate and kept up to date. The Perfect Candidate Should Have: • Proficient in Microsoft Office • Excellent organisational skills with the ability to multitask. • Exceptional accuracy and attention to detail with both written communication and numerical data. • Ability to prioritise workload and meet deadlines. • Good communication skills, both written and verbal. • Good numeracy skills and confidence working with stock quantities, prices and orders. Why Join Moulton Bulb Company?: In addition to a competitive salary we offer • Competitive company pension scheme • On-site staff canteen • Free, convenient on-site parking • Compassionate paid bereavement leave • Company sick pay • 24/7 Employee Assistance Programme & DoctorLine access • Long service rewards and recognition • Christmas gift voucher as a thank you from us • Supportive family-run business that values its people • Savings and cashback offers through the exclusive Moulton Bulb discount platform "Shallot More" • Free access to a comprehensive wellbeing hub • Committed to providing training and development opportunities • Clear career progression pathways and internal promotion opportunities If you are looking to make your mark and grow with a company that values its employees, we’d love to hear from you!

Read more and apply

Engineering · Full Time, Permanent

Engineering Lead Nights

Nights
Competitive Salary + Benefits4 on 4 offShift times: 18:00 - 06:00

An Engineering Lead responsible for leading and supporting the engineering team to deliver effective proactive and preventative maintenance, ensuring equipment reliability, efficiency, and compliance with food safety and quality standards. Working closely with operations and management, the role helps resolve equipment issues, supports continuous improvement, and ensures all engineering activities meet BRC, customer, and Health & Safety requirements The Position: • Oversee and guide the engineering team, ensuring effective support in the delivery of daily engineering activities. • Support the engineering team to meet proactive and preventative maintenance requirements • Work closely with the Packhouse Manager, Team Leaders and Line Leaders to understand, investigate, and rectify running issues to ensure that we achieve maximum efficiency from our equipment • Gain exposure and training to develop and maintain standard operating procedures (SOPs) in conjunction with the training team for engineering processes • Identify areas for improvement and escalate issues to ensure processes are up-to-date, properly trained, and consistently followed • Ensure completion of all maintenance, servicing and calibration requirements on factory equipment and associated documentation as required • Conduct risk assessments where appropriate prior to engineering works taking place onsite to ensure food safety • Manage and supervise external contractors working onsite ,ensuring policy and procedural requirements are communicated and adhered to at all times • Arrange and perform the regular maintenance of the fire alarm aspiration system • Assist in addressing faults and false alarms reported from the site fire alarm system • Actively seek to reduce supplier and service costs while maintaining quality standards. • Assist in the commissioning and installation of new machinery or factory refurbishments The Perfect Candidate Should Have: • Multi skilled engineer with a proven ability to work in a fast-paced environment • Project manager with the ability to efficiently prioritise workload to optimise performance • Ability to manage and liaise with a variety of cross-functional team members • Ability to effectively organise/schedule work to minimise downtime Why Join Moulton Bulb Company?: In addition to a competitive salary, we offer • Competitive company pension scheme • On-site staff canteen • Free, convenient on-site parking • Compassionate paid bereavement leave • Company sick pay • 24/7 Employee Assistance Programme & DoctorLine access • Long service rewards and recognition • Christmas gift voucher as a thank you from us • Supportive family-run business that values its people • Savings and cashback offers through the exclusive Moulton Bulb discount platform "Shallot More" • Free access to a comprehensive wellbeing hub • Committed to providing training and development opportunities • Clear career progression pathways and internal promotion opportunities If you are looking to make your mark and grow within a company that values it’s employees, we’d love to hear from you!

Read more and apply

Quality · Full Time, Permanent

QC

Days
£14.204 on 4 offShift times: 05:30 - 17:30

We are looking for a QC to ensure customer requirements and standards are achieved by providing an effective and efficient quality control service ‍The Position: ‍‍Undertake quality and label checks in the Grader, record findings and highlight any discrepancies to relevant department managers. Ensure accurate checking of codes/dates/promotional labels on our system. Take reference photos to support legal compliance and ensure product traceability is followed throughout the process. Inspect the quality of raw material against relevant specifications, and if required, explain the specification to other employees. Some inspections will be carried out off site. Communicate effectively with internal departments on quality issues to ensure prompt action is taken and notify the department managers of any quality or processing concerns. Provide our customers with products that meet their specification at all times Work together with the quality team to implement corrective action to improve the quality of the product to within specification Keep your work area in a good, clean condition and follow the clean as you go procedure Perform various tasks required during start-up checks, including shelf-life verification, scale checks, document control, and reviewing procedures and processes. Undertake any other reasonable duties as may be requested by your Manager to ensure the overall smooth running of the business The Perfect Candidate should have: ‍‍Previous QC experience within the food industry (preferable) Full UK driving licence Methodical with attention to detail Ability to work independently and as part of team Good basic understanding of English, both written and verbal Ability to carry out basic tasks on a computer or hand-held device Why Join Moulton Bulb Company? ‍In addition to a competitive salary and pension, we offer Competitive company pension scheme On-site staff canteen Free, convenient on-site parking Compassionate paid bereavement leave Company sick pay Premium overtime pay at 1.33 x your hourly rate 24/7 Employee Assistance Programme & Doctor Line access Long service rewards and recognition Christmas gift voucher as a thank you from us Supportive family-run business that values its people Savings and cashback offers through the exclusive Moulton Bulb discount platform "Shallot More" Free access to a comprehensive wellbeing hub Committed to providing training and development opportunities Clear career progression pathways and internal promotion opportunities If you are looking to make your mark and grow with a company that values its employees, we’d love to hear from you!

Read more and apply

Quality · Full Time, Permanent

QC Nights

Nights
£15.204 on 4 offShift times: 17:30 - 05:30

We are looking for a QC to ensure customer requirements and standards are achieved by providing an effective and efficient quality control service ‍The Position: ‍‍Undertake quality and label checks in the Grader, record findings and highlight any discrepancies to relevant department managers. Ensure accurate checking of codes/dates/promotional labels on our system. Take reference photos to support legal compliance and ensure product traceability is followed throughout the process. Inspect the quality of raw material against relevant specifications, and if required, explain the specification to other employees. Communicate effectively with internal departments on quality issues to ensure prompt action is taken and notify the department managers of any quality or processing concerns. Provide our customers with products that meet their specification at all times Work together with the quality team to implement corrective action to improve the quality of the product to within specification Keep your work area in a good, clean condition and follow the clean as you go procedure Perform various tasks required during start-up checks, including shelf-life verification, scale checks, document control, and reviewing procedures and processes. Undertake any other reasonable duties as may be requested by your Manager to ensure the overall smooth running of the business The Perfect Candidate Should Have: ‍‍Previous QC experience within the food industry (preferable) Methodical with attention to detail Ability to work independently and as part of team Good basic understanding of English, both written and verbal Ability to carry out basic tasks on a computer or hand-held device Why Join Moulton Bulb Company? ‍In addition to a competitive salary and pension, we offer Competitive company pension scheme On-site staff canteen Free, convenient on-site parking Compassionate paid bereavement leave Company sick pay Premium overtime pay at 1.33 x your hourly rate 24/7 Employee Assistance Programme & Doctor Line access Long service rewards and recognition Christmas gift voucher as a thank you from us Supportive family-run business that values its people Savings and cashback offers through the exclusive Moulton Bulb discount platform "Shallot More" Free access to a comprehensive wellbeing hub Committed to providing training and development opportunities Clear career progression pathways and internal promotion opportunities If you are looking to make your mark and grow with a company that values its employees, we’d love to hear from you!

Read more and apply

Engineering · Full Time, Permanent

Mechanical and Electrical Engineer

Nights
£38k - £46.5k +Night Premium £2098 pa depending on qualifications and experience4 on 4 offShift times: 18:00 - 06:00

We are looking for an engineer to perform reactive and preventative maintenance to ensure machinery operates at peak efficiency without compromising quality. Collaborate closely with site Technicians and Line Leaders to ensure all equipment remains fully operational and is maintained in line with company standards. You may already be a qualified engineer, or you may come from a car mechanic, plant fitter or similar hands on background. If you are mechanically minded, methodical and keen to learn, we will give you the training and funded qualifications to build a real career in our engineering team. ‍The position: Perform planned preventative maintenance across the site to minimise downtime. Resolve breakdowns and issues promptly and effectively, minimising impact on production. Recommend solutions aligned with the engineering strategy to reduce downtime. Identify areas for improvement in machine performance. Complete maintenance, servicing and general duties, escalating issues to the Engineering Lead/Supervisor where required. Work closely with the Engineering Supervisors to minimise equipment and tool purchases while ensuring all necessary tasks are effectively completed. Work closely with the Engineering Supervisors, Engineering Manager,Grader Manager, Line Leaders, machinery suppliers and manufacturers to ensure maximum efficiency is achieved. Ensure effective and timely resolution of breakdowns and issues, with minimal impact on production. Supervise external contractors working onsite, ensuring policies and procedures are communicated and always followed. Complete engineering paperwork accurately and competently to support compliance and audit readiness. Work closely with Engineering Team Leaders/Supervisors to minimise equipment and tool purchases while ensuring required tasks are completed effectively. Help the engineering leadership team to identify any parts/items required for repair or service. To book out and restock when required, parts held in the site engineering stores. Ensure all areas are clean and tidy at the end of shift. Maintain detailed records of all engineering tasks to support audit compliance. ‍The Perfect Candidate Should have: Experienced engineer with a mechanical and electrical engineering qualification desirable though we can provide training and funded qualifications for the right person. Confident working on their own and as part of a team. Can-do mindset to problem solving. Strong problem-solving skills, with the ability to identify the root causes and resolve issues. Proven organisational skills. Able to communicate clearly and effectively at all levels. Preferable industry knowledge: experience working in food manufacture industry. Self-driven, self-motivated and enthusiastic. Flexible working approach and ability to adapt to change Why join Moulton Bulb Company? In addition to a competitive salary we offer Competitive company pension scheme On-site staff canteen Free, convenient on-site parking Compassionate paid bereavement leave Company sick pay 24/7 Employee Assistance Programme & Doctor Line access Long service rewards and recognition Christmas gift voucher as a thank you from us Supportive family-run business that values its people Savings and cashback offers through the exclusive Moulton Bulb discount platform "Shallot More" Free access to a comprehensive wellbeing hub Committed to providing training and development opportunities Clear career progression pathways and internal promotion opportunities If you are looking to make your mark and grow with a company that values its employees, we'd love to hear from you!

Read more and apply

Packhouse · Full Time, Permanent

Line Leader

Days
£14.204 on 4 offShift times: 06:15 - 18:30

A Line Leader for our Packhouse to take responsibility for both staff and equipment within a defined area of the packhouse, ensuring the team achieve the daily production plan as scheduled by the planning team. ‍The Position: Carry out checks before packing and clean-down on uniform and jewellery Carry out check-weigher checks on time and correctly, reporting any issues found immediately Work with the supervising team, ensure that you have sufficient people to pack the relevant product Monitor top-tailer usage ensuring that they are working effectively Check that all packaging and labels used are correct, undamaged and meet quality standards Constantly monitor and ensure that the quality of the finished product meets specification. Any issues feedback to colleagues and soon as possible Monitor rejects, feeding back to colleagues if problems are found Turn off “moving” machinery at break times and turn off completely at the end of the working day Completely run the line out at the end of the working day, if agreed with the supervisors the hopper can be turned off and left full Provide cover for colleagues if they leave the line At the end of the day thoroughly check the line for any foreign objects and remove (wood, stones etc)· Any issue with your line must be reported to a supervisor or one of the engineering team Keep your work and surrounding areas clean, tidy and safe at all times Undertake any other reasonable duties as may be requested by your manager to ensure the overall smooth running of the business The Perfect Candidate Should Have: Ability to organise and prioritise workload as the situation requires Keen eye for detail Strong communication skills Ability to problem solve Proactive approach to work Ability to work as a team Why Join Moulton Bulb Company? In addition to a competitive salary, we offer On-site staff canteen Competitive company pension scheme Free, convenient on-site parking Compassionate paid bereavement leave Company sick pay Premium overtime pay at 1.33 x your hourly rate 24/7 Employee Assistance Programme & Doctor Line access Long service rewards and recognition Christmas gift voucher as a thank you from us Supportive family-run business that values its people Savings and cashback offers through the exclusive Moulton Bulb discount platform "Shallot More" Free access to a comprehensive wellbeing hub Committed to providing training and development opportunities Clear career progression pathways and internal promotion opportunities If you are looking to make your mark and grow with a company that values its employees, we'd love to hear from you!

Read more and apply

Goldwood · Full Time, Permanent

General Operative

Days
£13.514 on 4 offShift times: 07:00 - 18:30

Motivated Factory Operatives to undertake various functions in order to fulfil orders as per customer specifications and standards The Position: Trim, peel, bag and pack onions and other product as guided by your Line Manager and as per customer specifications Report any issues with machinery, product quality or packaging issues to your Line Manager Ensure packaging is not damaged when packing produce Assist management to meet and maintain the requirements of the BRC standard Ensure that the product that we pack for our customers is of the expected quality The Perfect Candidate Should Have: Good attention to detail Ability to work well with others Good verbal communication skills Why Join Moulton Bulb Company? ‍In addition to a competitive salary, we offer Competitive company pension scheme On-site staff canteen Free, convenient on-site parking Compassionate paid bereavement leave Company sick pay Premium overtime pay at 1.33 x your hourly rate 24/7 Employee Assistance Programme & Doctor Line access Long service rewards and recognition Christmas gift voucher as a thank you from us Supportive family-run business that values its people Savings and cashback offers through the exclusive Moulton Bulb discount platform "Shallot More" Free access to a comprehensive wellbeing hub Committed to providing training and development opportunities Clear career progression pathways and internal promotion opportunities If you are looking to make your mark and grow with a company that values its employees, we'd love to hear from you!

Read more and apply

Grader · Full Time, Permanent

General Operative

Days
£13.014 on 4 offShift times: 05:45 - 17:30

Inspect products as they move along the production line and remove any items that fail to meet quality standards Operate barcode scanners to track products entering and exiting production lines as required Maintain cleanliness throughout production by following “clean as you go” procedures, ensuring all debris is removed during, between, and after production runs Assist with setting up the grading line when needed, including operating machinery such as screens and topper beds in accordance with Standard Operating Procedures (SOPs) Potential occasional forklift support as required (training can be provided for suitable candidates) The Perfect Candidate Should Have: Thorough with strong attention to detail Ability to work well with others Why Join Moulton Bulb Company? In addition to a competitive salary, we offer Competitive company pension scheme On-site staff canteen Free, convenient on-site parking Compassionate paid bereavement leave Company sick pay Premium overtime pay at 1.33 x your hourly rate 24/7 Employee Assistance Programme & Doctor Line access Long service rewards and recognition Christmas gift voucher as a thank you from us Supportive family-run business that values its people Savings and cashback offers through the exclusive Moulton Bulb discount platform "Shallot More" Free access to a comprehensive wellbeing hub Committed to providing training and development opportunities Clear career progression pathways and internal promotion opportunities If you are looking to make your mark and grow with a company that values its employees, we'd love to hear from you!

Read more and apply

Grader · Full Time, Permanent

Forklift Driver

Days
£13.91 - £14.714 on 4 offShift times: 05:15 - 17:30

We are looking for a Forklift Driver to support grading operations by safely and efficiently transporting product, bins, pallets, and materials to and from the grading lines, hopper rooms, and storage areas. The role ensures smooth grading runs by maintaining accurate bin handling, weight checks, line supply, and adherence to food safety, quality, and health & safety standards. ‍The Position: Carry out daily forklift checks and routine maintenance including cleaning, water, oil, diesel and tyre pressure. Check empty bins before placing them onto the grading line to ensure they are clean, undamaged and fit for use. Remove full bins off the grading line promptly and transport them to the correct storage area. Check full bins containing product on the scales to ensure weights are accurate before labelling. Apply or support correct labelling procedures once weight accuracy has been confirmed. Transport graded product to designated storage locations in an organised and timely manner. Move product into hopper rooms in preparation for upcoming grading runs, ensuring correct product type and rotation. Support graders and line operators by responding quickly to bin, product, or hopper requirements to minimise downtime. Operate forklift trucks safely at all times in line with company procedures, site rules, and health & safety legislation. Immediately report any defects, faults, or safety concerns with forklifts or equipment to the Production Technician Engineer and/or Production Technician Supervisor. Ensure loads are secure, stable, and correctly positioned before lifting or transporting. Remain aware of pedestrians, machinery, buildings, and grading equipment to avoid damage or injury. Report all accidents, near misses, or incidents to the supervisor as soon as possible. Keep the grader area, forklift routes, and storage areas clean, tidy, and safe at all times. Stack bins, pallets, and trays neatly, in designated locations, and to the correct height. Complete all required paperwork fully and accurately, including forklift check sheets, loading plans, rejects records, hopper sheets, and any grader-related documentation. ‍The Perfect Candidate Should Have: Valid Counterbalance B1 forklift licence essential. Ability to prioritise tasks and problem solve. Ability to assess weights and judge distances and heights. Willingness to work in varying temperatures, depending upon season. Why Join Moulton Bulb Company? In addition to a competitive salary, we offer Competitive company pension scheme. On-site staff canteen. Free, convenient on-site parking. Compassionate paid bereavement leave. Company sick pay. Premium overtime pay at 1.33 x your hourly rate. 24/7 Employee Assistance Programme & DoctorLine access. Long service rewards and recognition. Christmas gift voucher as a thank you from us. Supportive family-run business that values its people. Savings and cashback offers through the exclusive Moulton Bulb discount platform "Shallot More". Free access to a comprehensive wellbeing hub. Committed to providing training and development opportunities. Clear career progression pathways and internal promotion opportunities. If you are looking to make your mark and grow with a company that values its employees, we'd love to hear from you!

Read more and apply

Grader · Full Time, Permanent

Forklift Driver Nights

Nights
£14.91 - £15.714 on 4 offShift times: 17:00 - 05:30

Are you an experienced forklift driver looking for a new opportunity where your skills truly make a difference? Join our nightshift grading team and play a vital role in keeping our operations running smoothly, safely, and efficiently. At Moulton Bulb Company, you won’t just be moving product—you’ll be a key part of a fast-paced, high-quality production environment where teamwork and precision matter. As a Night Shift Forklift Driver, you’ll support grading operations by transporting product, bins, pallets, and materials between grading lines, hopper rooms, and storage areas. Your work will ensure seamless production flow and help maintain our high standards of quality and safety. The Position: Carry out daily forklift checks and basic maintenance (cleaning, fluids, tyre pressure) Inspect empty bins to ensure they are clean, safe, and fit for use Remove full bins from grading lines and transport them to correct storage locations Accurately check product weights using scales before labelling Support and ensure correct labelling procedures Supply grading lines and hopper rooms with the right product at the right time Respond quickly to team needs to minimise downtime Operate forklift trucks safely in line with site rules and Health and Safety regulations Report any faults, defects, or safety concerns immediately Maintain awareness of surroundings to prevent accidents or damage Keep work areas clean, tidy, and organised Stack bins, pallets, and trays safely and correctly Complete all required documentation accurately The Perfect Candidate Should Have: Valid Counterbalance B1 Forklift Licence Strong coordination and spatial awareness Ability to assess weights, distances, and heights confidently A proactive, safety-first mindset Ability to work in varying temperatures depending on the season Team player with a reliable and flexible approach Why Join Moulton Bulb Company? ‍ In addition to a competitive salary, we offer Competitive company pension scheme On-site canteen Free, convenient on-site parking Compassionate paid bereavement leave Company sick pay Premium overtime pay at 1.33 x your hourly rate 24/7 Employee Assistance Programme and Doctor Line access Long service rewards and recognition Christmas gift voucher as a thank you from us Supportive family-run business that values it's people Savings and cashback offers through the exclusive Moulton Bulb discount platform "Shallot More" Free access to a comprehensive wellbeing hub Committed to providing training and development opportunities Clear career progression pathways and internal promotion opportunities If you are looking to make your mark and grow with a company that values its employees, we'd love to hear from you!

Read more and apply

Packhouse · Full Time, Permanent

General Operative

Days
£13.014 on 4 offShift times: 06:45 - 18:30Closes 29 Jan

Pack onions and other products as guided by your Line Leaders/ Team Leaders. Ensure all packaging is checked and is not damaged (i.e. split seals, damaged net etc) Ensure the produce is packed correctly and of the expected quality, removing any defective items from the line Moving product which involves lifting up to 17kg, carrying, pushing and pulling trays/product Ensure the packaging trays are clean and not broken, and that your work area is clean and tidy. Ensure that both hand and automatic clippers are operated in a safe manner and any issues are reported immediately Product dressing - if you are unable to dress the product to the required standard, stop the line and inform your Line Leader The perfect candidate should have: Ability to lift heavy objects and perform physical tasks as required Thorough with string attention to detail Flexible and open to change situations. Good coordination and dexterity. Excellent verbal communication skills. Why Join Moulton Bulb Company? ‍In addition to a competitive salary, we offer Competitive company pension scheme On-site canteen Free, convenient on-site parking Compassionate paid bereavement leave Company sick pay Premium overtime pay at 1.33 x your hourly rate 24/7 Employee Assistance Programme and Doctor Line access Long service rewards and recognition Christmas gift voucher as a thank you from us Supportive family-run business that values it's people Savings and cashback offers through the exclusive Moulton Bulb discount platform "Shallot More" Free access to a comprehensive wellbeing hub Committed to providing training and development opportunities Clear career progression pathways and internal promotion opportunities If you are looking to make your mark and grow with a company that values its employees, we'd love to hear from you!

Read more and apply

Talent pool

Join our talent pool

Nothing that fits today? Leave your details and CV and we will call you when the right role opens.
Job alerts

Be first to hear about new vacancies. No spam, unsubscribe any time.

We only use your email to tell you about new vacancies. Unsubscribe any time.

The range of careers

Agronomy & raw material

Work with growers on variety, nutrition, storage and crop health, backed by live university research.

Engineering

Keep a high-throughput packhouse moving and build the automation reshaping how we work.

Technology & data

Live operational data, tools we build ourselves, and real problems worth solving.

Commercial

Manage relationships with some of the UK's biggest retailers.

Operations

Grading, packing, planning and logistics. The engine room.

Quality & technical

Food safety and standards in a BRCGS AA+ site.

01

More ownership

Smaller team, wider remit. You will own things end to end rather than a narrow slice of a process.

02

More impact

What you do is visible. Good work gets seen, and it changes how the business runs.

03

Long-term thinking

No external shareholders, no quarterly-earnings treadmill. We back long bets and invest in people.

04

Real expertise

Because we specialise, the knowledge in this building runs deep.

Our people, their words

David Sobczak, Raw Materials Manager

David Sobczak · Raw Materials Manager

David joined in 2011 as a General Operative on a production line. Dedication, curiosity and hard work took him step by step to running raw materials for the whole business.

If you show initiative, put in the work and have a real interest in the business, the sky is the limit.

Watch David's story

HR Apprentice

There are so many opportunities. There are many different departments and we need more people who have the drive and desire to learn. Moulton Bulb has given me so many opportunities to try new things.

Hannah Evans · HR Apprentice

Hannah joined in July 2013, straight from school, for what she thought was a summer job, describing herself then as really shy. She stayed part-time right through university, with managers happy for her to work two or three days a week and through the holidays. She learnt the admin roles in 2017, became a Line Leader and Printroom Operative in 2019, trained new starters one to one after finishing her studies in 2020, and in March 2021 stepped into her HR Apprentice role.

Good to know